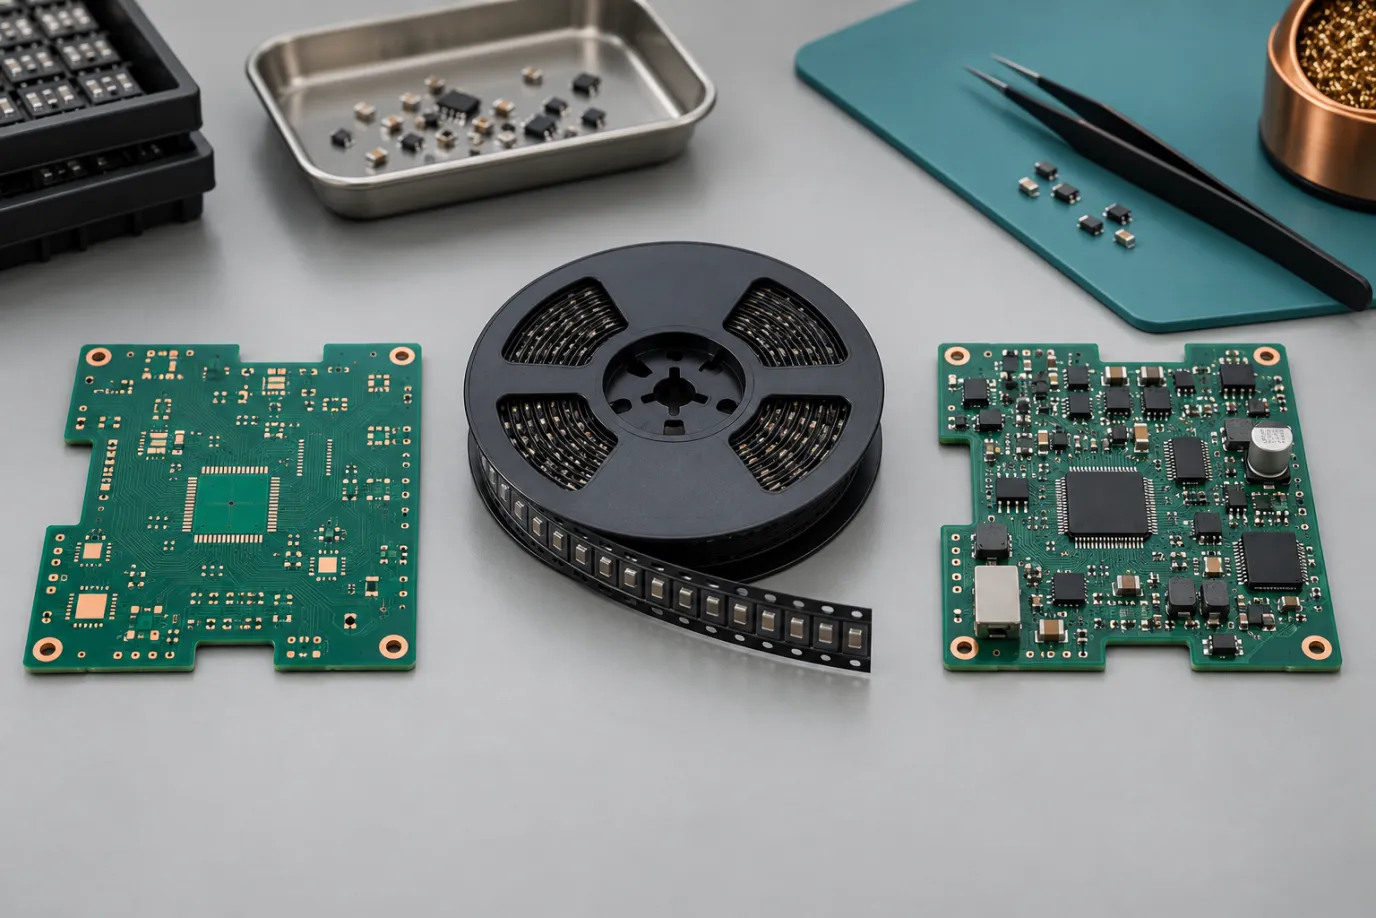
Turnkey PCB assembly is attractive because one supplier can coordinate several activities that would otherwise require separate conversations: bare-board fabrication, component purchasing, assembly, and agreed inspection or testing. For a small engineering team, that can reduce administrative work and make project status easier to follow. It can also expose unclear assumptions if everybody believes someone else owns the difficult decisions.
The word “turnkey” does not define every deliverable. One quote may include component sourcing and assembly but exclude programming. Another may include a functional test only after the customer provides a fixture and procedure. Before comparing prices, define the actual scope and assign responsibility for the decisions that affect quality, cost, and schedule. A clear handoff makes an integrated service useful; the label alone does not.
Start with a scope that names the finished deliverable
Describe what should arrive at the receiving dock. Is it an assembled board, a programmed and tested board, or a complete unit with cables and an enclosure? Identify any required labeling, coating, calibration, packaging, or documentation. These activities are easy to overlook when the initial conversation focuses only on component placement.
Specify quantities by configuration. A purchase order for several variants should identify how many of each are needed and how they differ. If the same PCB supports multiple populations or software versions, the supplier needs a controlled way to distinguish them through production and shipment.
Also identify what the supplier is not being asked to design. A build-to-print service generally relies on customer-defined requirements. If design review, circuit changes, or test development are needed, describe those tasks explicitly rather than assuming they are included in routine assembly engineering.
Name the owner of the release package
One person or team should authorize the manufacturing package. That package can include fabrication data, drawings, stackup requirements, BOM, placement data, assembly instructions, firmware, and test documents. The exact contents depend on the product, but the revision relationship between them must be clear.
A release manifest helps prevent partial updates. List the approved files, their revisions, and any exceptions that remain open. If the BOM changes but the assembly drawing does not, state whether that is intentional. A supplier should not need to infer the approved configuration from several overlapping emails.
Define how questions are routed. Routine manufacturing clarifications may go to one engineer, while substitutions or functional changes may require a different approval. Giving the supplier a response path is as important as giving it the files, especially when purchasing commitments are waiting on an answer.
Separate manufacturability advice from design approval
Manufacturers may propose changes to improve fabrication or assembly. Examples include a panel adjustment, a different tooling arrangement, or an alternative material construction. These suggestions can be valuable, but they do not transfer ownership of the product’s performance requirements.
Agree on what the supplier can adjust within an approved process and what requires written customer approval. A change that seems small in production may affect impedance, mechanical fit, component clearance, or a customer requirement. The approval should describe the exact change and the revision or batch to which it applies.
Reviewing PCB fabrication capabilities early helps identify which features need a specific engineering discussion. It is better to confirm the required construction before placing component orders than to discover that the board needs redesign after material has been committed.
Establish purchasing and substitution rules
Identify the sourcing model for each category of material. The supplier may buy all components, the customer may consign selected items, or the project may use a hybrid arrangement. Include custom parts and mechanical items instead of limiting the discussion to standard electronic components.
The BOM should distinguish approved alternatives from proposed replacements. An assembly supplier can identify an availability problem and suggest candidates, but technical equivalence requires the appropriate review. Define who can authorize a replacement, what evidence is required, and whether the approval is temporary or permanent.
Also agree on acceptable supply channels and any required traceability. These requirements affect purchasing options and should be part of the quotation basis. If a shortage forces a different source proposal, the supplier should raise it as an exception rather than silently changing the agreed approach.
Decide who carries inventory exposure
Component ordering can create obligations beyond the quantity installed on the boards. Minimum purchase quantities, packaging increments, setup allowances, and non-cancelable commitments can leave material after the build. A lower component unit price may also require a larger purchase.
Agree on authorization limits before the supplier commits to those costs. Define ownership of unused material, storage arrangements, and the treatment of excess or obsolete stock following a design change. If the next production order is uncertain, do not assume that future consumption will solve today’s inventory question.
For customer-supplied parts, define delivery timing and receiving requirements. The production schedule may depend on having the complete usable kit available. A shipment that arrives on time but contains unidentified or unsuitable material does not necessarily make the build ready to start.
Build the schedule around release conditions
Ask what event starts the quoted manufacturing lead time. It may depend on approved data, payment, complete material availability, or resolution of engineering questions. These conditions should be visible when comparing quotations.
A practical schedule includes milestones for technical review, material confirmation, fabrication, assembly, testing, and shipment. Some activities may overlap, but the dependencies still matter. A component can arrive early while an unresolved stackup question prevents the board from being released.
Use a short list of open issues with an owner and due date. This is more actionable than repeatedly requesting an overall completion percentage. A single unapproved connector substitution can be more important than many completed administrative tasks.
Specify inspection, testing, and programming separately
Inspection, electrical testing, and functional testing answer different questions. Identify which activities are included, what criteria apply, and what records are required. Avoid relying on the phrase “fully tested” unless the actual scope is attached.
Programming also needs a defined process. Provide the authorized software release, the method for verifying it, and any rules for unique device data. If a test procedure requires special fixtures, loads, or host software, assign responsibility for providing and maintaining them.
When comparing turnkey PCB assembly arrangements, ask for these responsibilities to be stated in the quotation or project agreement. This allows an integrated service to be evaluated on the work it will actually perform, including the tasks that are often omitted from a simple board price.
Plan the first build as a controlled learning step
A pilot build can reveal problems in instructions, handling, assembly sequence, or testing that were not obvious during design review. Decide beforehand what must be learned and what evidence will be reviewed before releasing a larger batch. The pilot should have a purpose beyond producing a few units quickly.
Record deviations and rework. A board that eventually passes after manual intervention may still indicate a process issue that will become expensive at volume. Separate the final number of acceptable units from the number that passed without repair or adjustment.
Agree on who approves progression to the next stage. Open issues may be acceptable for limited engineering use but unacceptable for customer shipment. The release decision should reflect that distinction rather than treating all successful power-on demonstrations as production approval.
Make changes traceable across every workstream
After a change is approved, identify its effect on boards, components, firmware, fixtures, and documents. A connector change may affect purchasing and mechanical fit; a pad change may affect fabrication, stencil data, and inspection programming. Updating one file does not guarantee that the rest of the process has followed.
Determine the cut-in point. State whether the change applies to the current batch, the next purchase order, or a defined serial-number range. Review work already completed and material already committed before deciding how to proceed.
Keep the as-built record with the shipment information. The intended configuration and the delivered configuration should be reconcilable, including any approved exceptions. This becomes especially important when the customer requests an identical repeat build months later.
Use a responsibility table before accepting the quote
A compact table can expose gaps without adding much paperwork. List each deliverable, its owner, the approval authority, and the condition that makes it complete. Typical rows include manufacturing data, BOM approval, component sourcing, panel approval, firmware, test procedure, failure disposition, and shipment release.
For example, the supplier may develop a panel proposal while the customer approves the board-edge constraints. The supplier may purchase components while the customer approves alternatives. Either arrangement can work if both sides understand it. Problems arise when coordination is mistaken for unlimited authority.
The most useful turnkey relationship gives the customer fewer interfaces while preserving clear decisions. Before production starts, both sides should be able to explain what will be delivered, which assumptions remain open, and who can resolve each one. That clarity makes schedules more credible and repeat orders easier to manage.